 A major PPE manufacturer has become the only one in the UK to use clean room technology in the production of high-grade medical masks for the NHS.
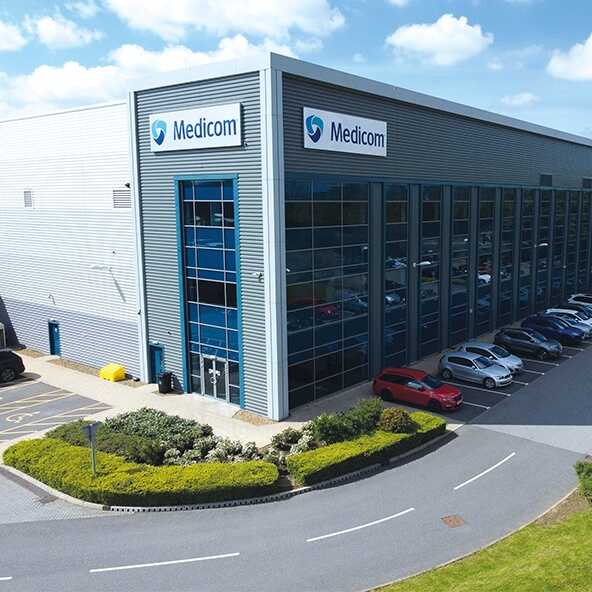
The Canadian-based group Medicom has created a state-of-the-art production facility in Northampton. It uses industry-leading technology which changes the air up to 20 times an hour.
The highly sterile environment exceeds the standards required for mask manufacturing. Medicom’s plant is making more than half a billion masks for the NHS through a government contract.
Covering more than 20,000 square feet, the clean room sits as an independent structure within the Medicom facility and is specially-designed to maximise hygiene. It means the supply of fresh air is highly filtered and ensures that no contaminants enter the manufacturing area.
Doors leading to the clean room are all equipped with airlock arrangements. The manufacturing space is positively pressured to 15 Pa (pascal) by a 100% fresh air system.
High Quality
The Northampton factory has created 250 new jobs. Medicom’s Managing Director in the UK, Hugues Bourgeois, said the company was proud to supply high-quality masks for the NHS using the latest technology.
“Our Northampton clean room is a great example of how technology can be used to help the medical profession deal with the continuing challenges of Covid.
“We are proud to be the only company in the UK using a clean room for the production of PPE masks. It underlines our commitment to supply products of the highest standards for NHS workers.”
Ideal Environment
Medicom strongly believes that all PPE should be created in a clean room environment to uphold high standards of manufacturing for clinical products.
For mask production, there are a number of key benefits – including less wastage, cost reduction, consistent quality and reliability. Many scientists have pointed out that it is the “chief strategy to combat contamination and particle-induced defects” .
High Efficiency Particulate Arrestors (HEPA) trap the smallest of particles that other air filtration systems would simply re-circulate into the air. At the same time, a consistent clean room condition of 20C and 50% RH (relative humidity) is maintained.
This ideal environment is achieved using a suite of recirculation air handling units (AHU’s). These units provide cooling and maintain an air exchange rate via filters of up to 20 air changes every hour.
With the air being filtered and changed so often, all airborne contaminants are removed from the manufacturing area. This ensures the production of the highest quality masks in terms of cleanliness, filtration efficiency and biocompatibility.
Laboratory Tested
Medicom’s FFP3 respiratory masks are made under the internationally renowned Kolmi brand and offer a high level of protection from aerosol generated infection. They have been specially created for use by NHS frontline workers.
The Kolmi Type II R Mask is popular with health professionals and is intended for all medical examinations. The mask has fluid resistant non-woven materials providing a barrier against spray, splatter and airborne particles.
The masks feature base materials produced by a world-leading manufacturer of non-woven and filter materials for the healthcare sector. Berry Global have a factory in South Wales, ensuring a secure UK supply chain.